
MaxiLobe
Get more from every production run with the Alfa Laval MaxiLobe® hygienic rotary lobe pumps. Engineered for higher efficiency, a broader operating range, and simplified maintenance, MaxiLobe helps reduce investment and operating costs while boosting yield. Reliable performance across varying process conditions supports more uptime, consistent product quality, and lower total cost of ownership across dairy, food, beverage, and home and personal care applications.
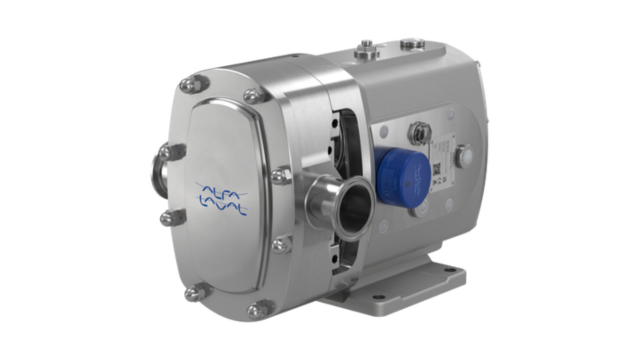
Outstanding reliability and performance for the hygienic industries
- Reduce investment costs, maximize process flexibility, and streamline system design
- Boost profitability and product quality through increased production efficiency and minimized downtime
- Safeguard product integrity, simplify process validation, and minimize cross-contamination risks with 3-A and EHEDG-certified pumps
- Simplify maintenance and maximize uptime due to front-loading seal, fully interchangeable spare parts and easy-to-set pump clearances
- Upgrade legacy rotary lobe pumps with minimal pipework modifications
With MaxiLobe sanitary rotary lobe pumps, you can tailor performance to meet your exact requirements, maximizing high production capacity while minimizing capital and operating costs. High volumetric efficiency and a wide performance envelope enable smaller, more cost-effective pumps to run at lower speeds, helping protect product quality while reducing product shear, energy use, and equipment wear.
With flow rates of up to 350 m3/h, pressure capabilities up to 16 bar, and 15 sizes, MaxiLobe gives you greater flexibility and more precise pump selection without the risk of oversizing. Each pump is fully factory-tested to ensure reliable performance, faster batch changeovers. Optional condition monitoring for predictive maintenance is available.
For Alfa Laval SRU pump upgrades, MaxiLobe hygienic rotary lobe pumps can provide at least 5% higher flow rates on a model-for-model basis, increasing throughput without process modifications.
Optimized investment
High volumetric efficiency and a wide performance envelope often allow for a smaller, more cost-effective pump while ensuring both production capacity and product quality. A broad range, flexible configurations, and compatibility with previous Alfa Laval models simplify pump selection and enable full-port dimensional interchangeability or similar.
Cost-effective operation
High volumetric efficiency enables lower operating speeds, ensuring gentle product handling, increased yield, and low energy consumption. Excellent cleanability and a robust design minimize downtime and increase production efficiency. Compatibility with previous Alfa Laval hygienic rotary lobe pumps enables a simple upgrade path to improved yield, product quality, and lower operating costs.
Enhanced assurance
Fully factory-tested and built on Alfa Laval’s proven rotary lobe technology, MaxiLobe pumps are designed for hygienic applications and offer excellent cleanability and reliable hygienic performance. MaxiLobe is certified by EHEDG- and 3-A, and it complies with FDA regulations. Optional ATEX-compliant models are available for use in explosive atmospheres.
Simpler service
A front-loading seal, fully interchangeable spare parts and easy-to-set pump clearances greatly simplify service. In many cases, the pump can be serviced without removal from the process line, which minimizes downtime and maintenance complexity. The optional Alfa Laval Clariot™ condition monitoring system further enhances reliability and enables optimized service intervals.
Maximizing flexibility in food and beverage production
See how MaxiLobe pumps maximize flexibility in modern food and beverage production. The exceptional volumetric efficiency allows the same pump to handle media with very different viscosities, making frequent product changeovers simple and efficient.
Ensuring quality in dairy production
Learn how MaxiLobe pumps ensure uniform concentration of suspended solids, such as cheese curd grains, supporting consistent product quality in dairy production. The tight design enables MaxiLobe pumps to handle a wide range of viscous media at high flow rates
Increasing efficiency in home and personal care production
Explore how MaxiLobe pumps increase productivity in home and personal care production. Efficient handling of media with widely varying viscosities, combined with fast cleaning between batches, enables quick turnarounds and maximum utilization of the main mixer.
How MaxiLobe rotary lobe pumps work
Alfa Laval MaxiLobe hygienic rotary lobe pumps are positive displacement pumps that provide smooth, reliable transfer of low- to high-viscosity products while maintaining product integrity.
Inside the pump head, precision-machined rotors rotate in opposite directions without contacting each other or the pump casing. A robust timing gearbox synchronizes the rotors, maintaining precise clearances throughout operation.
As the rotors turn, cavities are created between the rotor lobes and the pump casing. These expanding cavities generate a partial vacuum at the inlet, drawing product into the pump. The product is then gently carried around the outside of the rotors within the cavities. As the rotors mesh on the discharge side, the cavities decrease in size, displacing the product through the outlet at a consistent flow rate.
Because there is no metal-to-metal contact within the pump head, MaxiLobe minimizes product shear and wear while delivering efficient, hygienic fluid transfer. The pump is therefore well suited for handling sensitive, shear-sensitive, and high-viscosity products across a wide range of hygienic processing applications.
Alfa Laval MaxiLobe FAQs
Q. How does MaxiLobe’s volumetric efficiency compare to that of Alfa Laval SRU and SX pumps?
A. In general, the MaxiLobe delivers higher volumetric efficiency than the equivalent Alfa Laval SRU and SX pump sizes. Depending on the duty point, the improvement is most noticeable in low-viscosity and/or high-pressure applications. Accurate comparison requires selecting the appropriate pump size and determining the expected operating speed for your application. Actual performance depends on your specific operating conditions.
Q. Can the MaxiLobe replace the Alfa Laval SRU and SX pumps?
A.The MaxiLobe matches the key porting dimensions of all Alfa Laval SRU pumps and most SX models, enabling replacement with minimal or no modification to existing pipework. To support evaluation and replacement planning, 3D CAD models are available.
Q. Is EN 10204 3.1 material traceability available for MaxiLobe?
A. Yes. EN10204 3.1 material traceability is available as an option.
Q. Is the Alfa Laval knife-edge shaft seal available for the MaxiLobe?
A. Yes. Developed specifically for demanding applications such as chocolate processing, the Alfa Laval knife-edge single shaft seal is available for MaxiLobe sizes 22~63. It requires no external flush media, helping simplify installation and reduce operating costs.
Q. What surface finish options are available for MaxiLobe?
A. MaxiLobe is available with an Ra 0.8 μm surface finish. For enhanced wear resistance, a diffusion hardened surface treatment is available for MaxiLobe sizes 22~73.
Q. Is ATEX certification available?
A. Yes. ATEX certification is available for MaxiLobe sizes 22~73. Alfa Laval can supply both bare-shaft and motorized pumps as ATEX-compliant for Group II, Category 2G, Zone 1 areas.
Q. Does a MaxiLobe pump used with the Alfa Laval ClariotTM condition monitoring system and an active subscription qualify for an extended or lifetime warranty for the pump?
A. A MaxiLobe pump can qualify for an extended warranty of up to 10 years, provided it is equipped with the Clariot condition monitoring solution and the monitoring service remains active for the entire warranty extension period.
Close at Hand 카탈로그
CAD portal
서비스
문의 사항이나 궁금한 점이 있으시면 언제든지 연락해 주시기 바랍니다.
The Alfa Laval Pump Handbook – New Edition
Get your free copy right away. Our popular 375-page Pump Handbook serves as a reference book for pump specialists and as textbook at technical universities. Prepared for specialists by specialists, the book is a valuable source of theory and practice, packed with specific examples from real-world applications and a whole section on pump troubleshooting. With new pump technologies and focus on high pump efficiency to save resources, the new edition of the Pump Handbook is available for free download.

애플리케이션 & 이노베이션 센터 둘러보기
설비 업그레이드를 결정하기 전, 귀사의 공정에 가장 적합한 최적의 장비를 찾고 실질적인 비용 절감 효과를 미리 검증하고 싶으신가요?
알파라발 Application & Innovation Center에서 이 모든 것을 직접 테스트하고 눈으로 확인하실 수 있습니다.
알파라발의 Optimize™
알파라발의 공정 최적화 솔루션인 Optimize™는 리스크 없는 최소한의 투자만으로 고객의 기존 공정 성능을 극대화합니다. 운영에 필수적인 물, 에너지 및 화학약품 사용량을 최대 90%까지 획기적으로 절감하여 경제성과 지속가능성을 동시에 실현합니다.